
Chemical Processing
Controlled Bulk Handling for Demanding Chemical Processes
From fine powders to granular materials, ISL Technologies engineers IBC and Cone Valve systems for the controlled storage, transfer, discharge, dosing and blending of chemical materials.
Improve material flow, strengthen containment and build greater control into your chemical production process.

 Controlled Material Flow
- Contained Handling
- Process Flexibility
Chemical Process Challenges
When Material Behaviour Meets Process Complexity
Chemical materials can present some of the most demanding bulk-solids handling conditions. Fine powders, difficult flow characteristics, blending requirements, cleaning demands and hazardous materials can all affect how efficiently a production process operates.
How ISL Helps
A More Controlled Way to Handle Chemical Powders
ISL Technologies combines IBC systems, patented Cone Valve Technology and supporting process equipment to create a controlled material path from storage through discharge and downstream processing.
Featured Solution
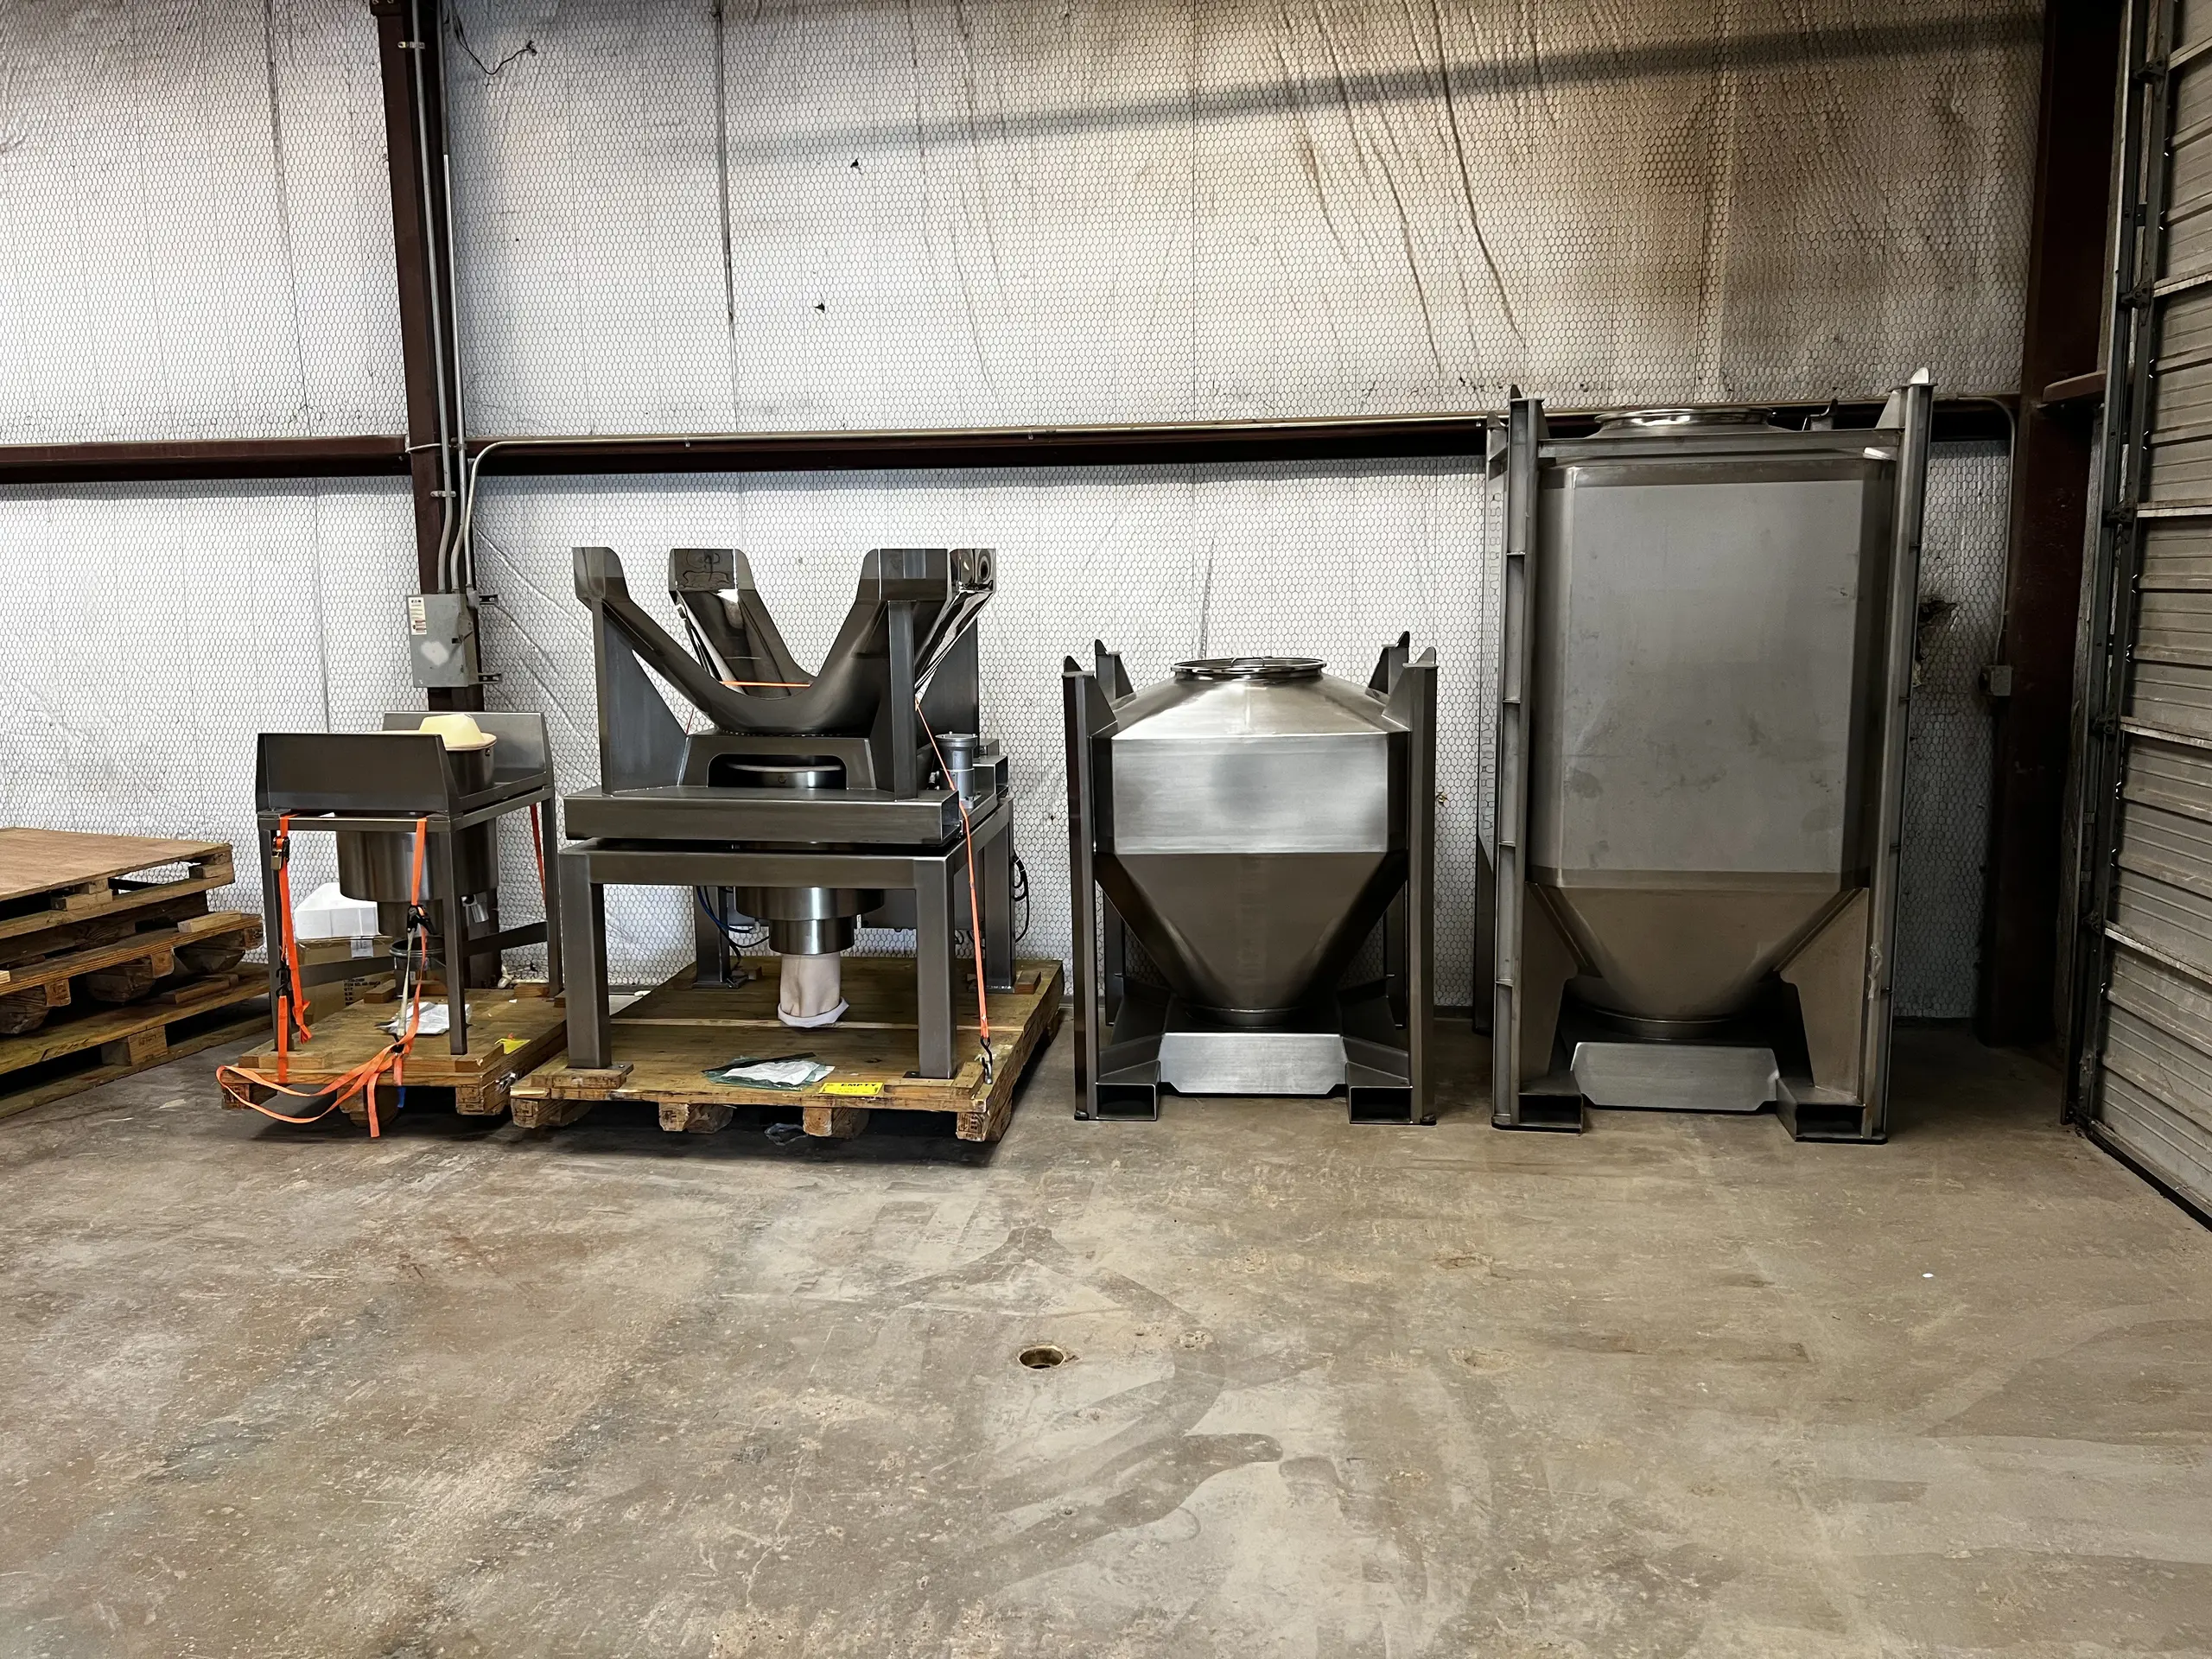
Controlled IBC Discharge
The ISL Cone Valve is designed to provide a variable aperture for controlled discharge of powders and granular materials.
By promoting a systematic flow pattern, the technology helps address common bulk-solids problems while providing controlled transfer from the IBC to the next stage of the process.
The technology is also designed to support containment, batch dosing and continuous dosing applications.


Contained Material Handling
Keep chemical powders and granular materials within a controlled material path during storage and transfer.

Controlled Discharge
Regulate material flow from the IBC using the variable aperture of the Cone Valve.

In-Bin Blending
Blend materials directly inside the IBC while reducing unnecessary product transfers.

Accurate Dosing
Use load-cell feedback and controlled valve movement for batch or continuous dosing applications.

Flexible IBC Handling
Use IBCs as identifiable batch vessels for storage, transport and in-process handling.

Cleaning & Changeover
Design the system around cleaning requirements to reduce unnecessary production downtime.
The Technology
Control Material Flow at the Source
Chemical powders do not always behave predictably when discharged from a storage vessel.
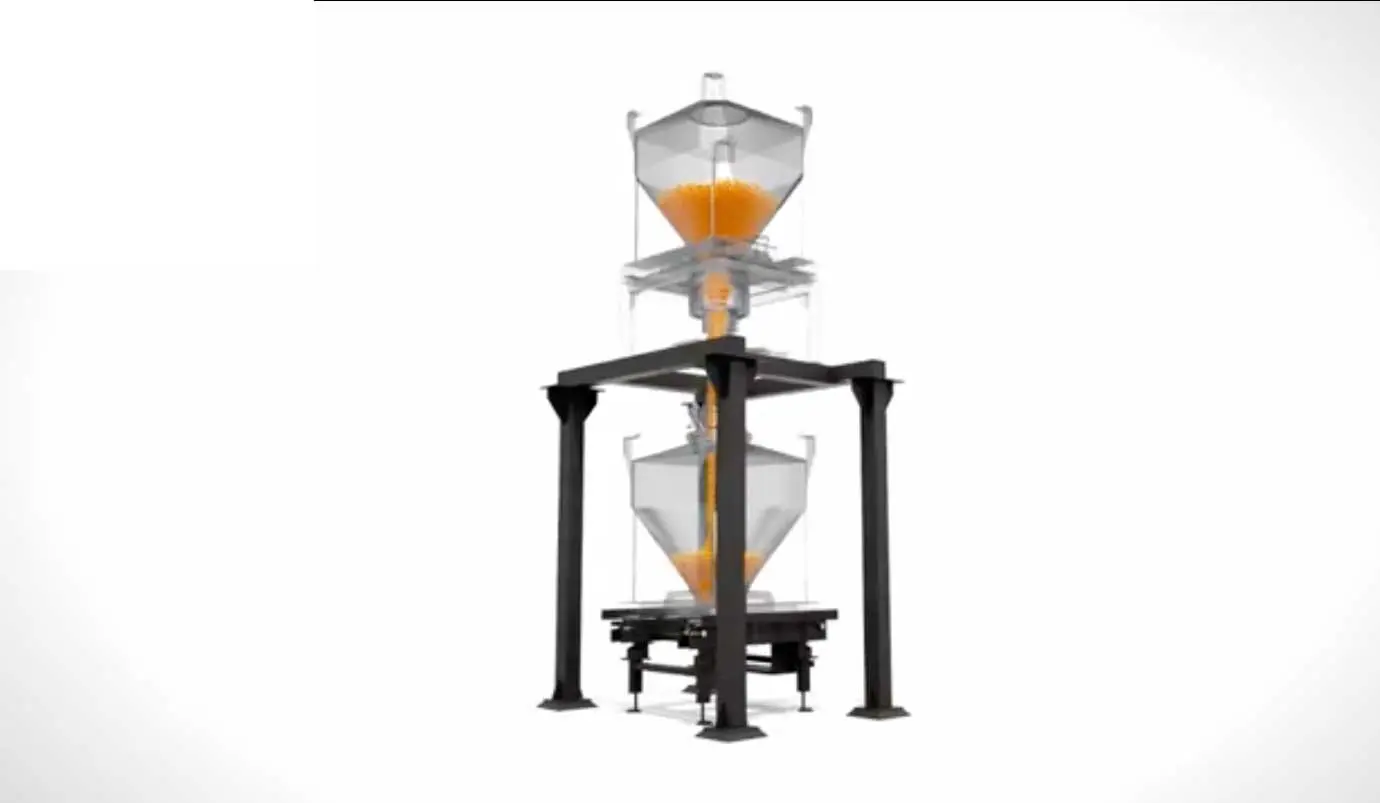
The ISL Cone Valve was developed to provide controlled discharge directly from the bulk store. Its variable aperture allows the flow of material to be adjusted according to the requirements of the process.

Mass Flow
Promotes a systematic first-in, first-out flow pattern through the bulk material.

Variable Flow Control
The valve aperture can be adjusted to control the material discharge rate.

Reduced Segregation
Systematic discharge helps minimise segregation when handling blended materials.

Contained Transfer
The Cone Valve integrates with the discharge station to support controlled material transfer.

Accurate Dosing
Load cells and feedback systems can be incorporated for batch and continuous dosing.

No Mechanisms in the Flow Path
The ISL technical material highlights the absence of mechanisms within the product flow path, helping reduce product damage, contamination and equipment wear.
Difficult Flow Applications
Designed for Materials That Don't Always Flow Easily
Fine and cohesive chemical powders can create serious problems during discharge. Bridging, rat-holing and inconsistent flow can interrupt production and require operator intervention.
ISL's Cone Valve approach is designed to promote mass flow while providing a controlled discharge path from the IBC.
For applications involving difficult-to-flow powders, the discharge station can also incorporate optional frame vibrators to help create material flow and support full discharge.

Promote Flow
Encourage consistent material movement from the IBC.

Control Discharge
Adjust the valve aperture according to process requirements.

Support Full Discharge
Optional vibration can assist with difficult-to-flow powders.
In-Bin Blending
Blend Chemical Formulations Directly Inside the IBC
When multiple chemical powders need to be combined, every additional transfer creates another handling stage.
ISL's In-Bin Blending system allows materials to be mixed directly inside the IBC.
As the IBC rotates, the patented Cone Valve lifts and drops to separate and re-mix the material, helping create a homogeneous blend while reducing the number of product transfers.

Reduced Product Transfers
Move the formulation through fewer process stages.
Contained Blending
Keep the material inside the IBC during the blending process.
Improved Blend Uniformity
The Cone Valve's re-mixing action is designed to help minimise segregation.

Flexible Batch Production
Use individual IBCs for different formulations and production batches.

Lower Changeover Burden
IBC-based blending can simplify the transition between different formulations.
Applications
Engineered for a Wide Range of Chemical Materials
ISL's bulk-solids technology can be configured for different powder, particulate and granular applications where controlled flow, containment and process efficiency are important.

Fine Chemical Powders
Controlled storage, discharge and dosing for fine and challenging powder materials.
Chemical Blends
Contained blending and discharge for multi-component formulations.
Detergent Materials
IBC-based handling and discharge for powdered detergent production.

Refractory Materials
Batching and controlled material handling for demanding refractory manufacturing processes.

Toner & Specialty Powders
Controlled discharge and dosing for specialised powder applications.

Industrial Chemicals
Flexible bulk handling systems designed around specific material and process requirements.
The ISL Difference
Engineering Control Into Every Stage of Material Handling
Chemical processing requires more than equipment that simply moves material. The system needs to account for flow behaviour, containment, cleaning, dosing, formulation and integration with the wider production process.
ISL combines Cone Valve Technology with application-specific engineering to address these requirements.
Controlled Flow
Variable Cone Valve aperture provides greater control over material discharge.
Containment
Designed to maintain a controlled material path and reduce product exposure.
Reduced Segregation
Systematic discharge helps maintain greater consistency when handling blended materials.
Accurate Dosing
Batch weighing and continuous dosing can be achieved through controlled discharge and feedback.

Simplified Cleaning
Equipment is designed around accessibility and simplified maintenance.

Process Integration
IBC systems can be integrated with supporting equipment such as silos, dust collectors, conveying systems and other process equipment.
From Storage to Process
One Connected System for Your Bulk Materials
ISL can integrate multiple stages of chemical material handling into an IBC-based workflow, reducing unnecessary transfers and giving manufacturers greater control over how materials move through production.

Fill
Load chemical powders or granular materials into the IBC through a controlled filling system.

Store
Keep the material within an identifiable IBC ready for transport or processing.

Blend
Combine ingredients directly inside the IBC when the formulation requires blending.

Move
Transport the IBC to the next production stage using its support structure and handling equipment.
Discharge
Connect the IBC to the discharge station and control material flow through the Cone Valve.
Dose
Use weighing or feedback-based control for batch or continuous dosing.

Clean
Clean and prepare the IBC for its next application according to the required process.
Contained Handling
Keep Material Where It Belongs
For chemical manufacturers, containment can be an important part of both process control and workplace safety.
ISL's IBC and Cone Valve approach is designed to minimise unnecessary exposure during material transfer, with contained filling and discharge options available as part of the wider system.

Contained Transfer
Reduce open handling between process stages.
Controlled Discharge
Manage the movement of material into the downstream process.

Reduced Product Exposure
Maintain a more controlled material path throughout discharge.
Cleaning & Changeover
Reduce the Time Between Production Runs
Cleaning can become a major source of downtime when manufacturing multiple chemical products or formulations.
An IBC-based process provides an opportunity to separate material handling and cleaning activities from the main production process. ISL can also engineer washing and drying systems according to the type of bulk solid being handled.

Accessible Equipment
Designed for straightforward dismantling and cleaning.

Reduced Downtime
Minimise the time equipment remains unavailable for production.

Flexible Changeovers
Prepare IBCs for subsequent materials and formulations.
Application-Specific Cleaning
Washing and drying systems can be designed around the material and process requirements.
Application in Action
Engineering Solutions for Real Chemical Processes
ISL Technologies has applied its bulk-solids handling technology to chemical manufacturing challenges involving batching, discharge, cleaning, maintenance and process efficiency.

Improving Batch Accuracy & Safety in Refractory Manufacturing
An ISL batching system achieved accuracy of ±0.1 lb for batch sizes up to 500 lb while improving product uniformity and operator safety.
Read Case StudyFaster, More Reliable IBC Discharge for Detergent Tablet Production
A standardised ISL approach supported faster delivery and reliable IBC discharge, with standard components available in 2–3 weeks and custom configurations in under six weeks.
Read Case StudyCone Valve Upgrade for Soap Production
An ISL Cone Valve upgrade addressed cleaning and maintenance challenges while reducing downtime and annual spare-parts costs.
Read Case StudyCone Valve Conversion for Toner Batching
An ISL Cone Valve conversion provided a user-friendly discharge solution that was rapidly adopted by operators.
Read Case StudyApplication Engineering
The Right Configuration Starts With Your Material
There is no single configuration for every chemical process.
Material characteristics, batch size, flow behaviour, production rate, containment requirements and downstream equipment all influence the final system.
ISL works with customers to determine the appropriate combination of IBCs, Cone Valve discharge, blending, dosing, conveying and supporting equipment.
Stainless Steel IBCs
For applications requiring durable stainless-steel construction.
Polyethylene IBCs
A practical alternative for applications where stainless steel is not required.
Discharge & Dosing
Controlled discharge for downstream mixing, packaging, screening or conveying.
In-Bin Blending
Direct blending inside the IBC.

Formulation Systems
Multi-ingredient batching and formulation systems.

Washing & Drying
IBC cleaning solutions designed around specific material requirements.
Engineering Knowledge
Explore Chemical Bulk-Handling Technology
Cone Valve Technology
Understand how controlled discharge and mass flow work.
Learn more
Discharge & Dosing
Explore controlled and accurate powder discharge.
Learn moreIn-Bin Blending
See how chemical formulations can be blended directly inside the IBC.
Learn moreIBC Systems
Explore IBC configurations for different bulk-solid applications.
Learn moreControl Systems
Learn how automation and feedback can be integrated into discharge and dosing.
Learn more
Case Studies
See how ISL has solved real bulk-solids challenges in chemical manufacturing.
Learn moreChemical Processing FAQ
Frequently Asked Questions
ISL systems are designed for powders, particulates and granular materials. The existing chemical offering specifically addresses challenging materials including ultra-fine powders and other bulk solids. The correct system configuration depends on the material's characteristics and process requirements.
Yes. Cone Valve Technology is designed to promote mass flow and address common bulk-solids flow issues such as bridging and rat-holing. Optional frame vibrators can also be incorporated for difficult-to-flow powders.
Yes. ISL's In-Bin Blending system allows materials to be blended directly inside the IBC. The Cone Valve's movement during blending helps separate and re-mix the material.
ISL's chemical-industry offering addresses the need for safe and contained handling of chemical materials. However, suitability for a specific hazardous material must be evaluated based on the material properties, process conditions and applicable safety requirements.
Yes. ISL systems can incorporate load cells and controlled Cone Valve movement for batch weighing and continuous dosing applications.
An IBC-based approach can reduce unnecessary transfers and allow cleaning and preparation activities to be managed independently of certain production stages. ISL also provides washing and drying systems designed around the material and application.
Yes. ISL's engineering capability can extend beyond the IBC to supporting equipment such as silos, dust collectors, conveying systems, conveyors and AGVs where required by the application.
Yes. ISL's current case-study portfolio includes chemical applications involving refractory manufacturing, detergent tablet production, soap production and toner batching.
Engineer Your Chemical Process
Let's Solve Your Bulk-Handling Challenge
Whether you're dealing with difficult powders, demanding flow requirements, formulation changes, cleaning downtime or controlled dosing, ISL Technologies can help engineer an IBC and Cone Valve solution around your process.
Tell us what material you're handling and where the challenge occurs.